Description
Traceable alloy butt-weld fitting
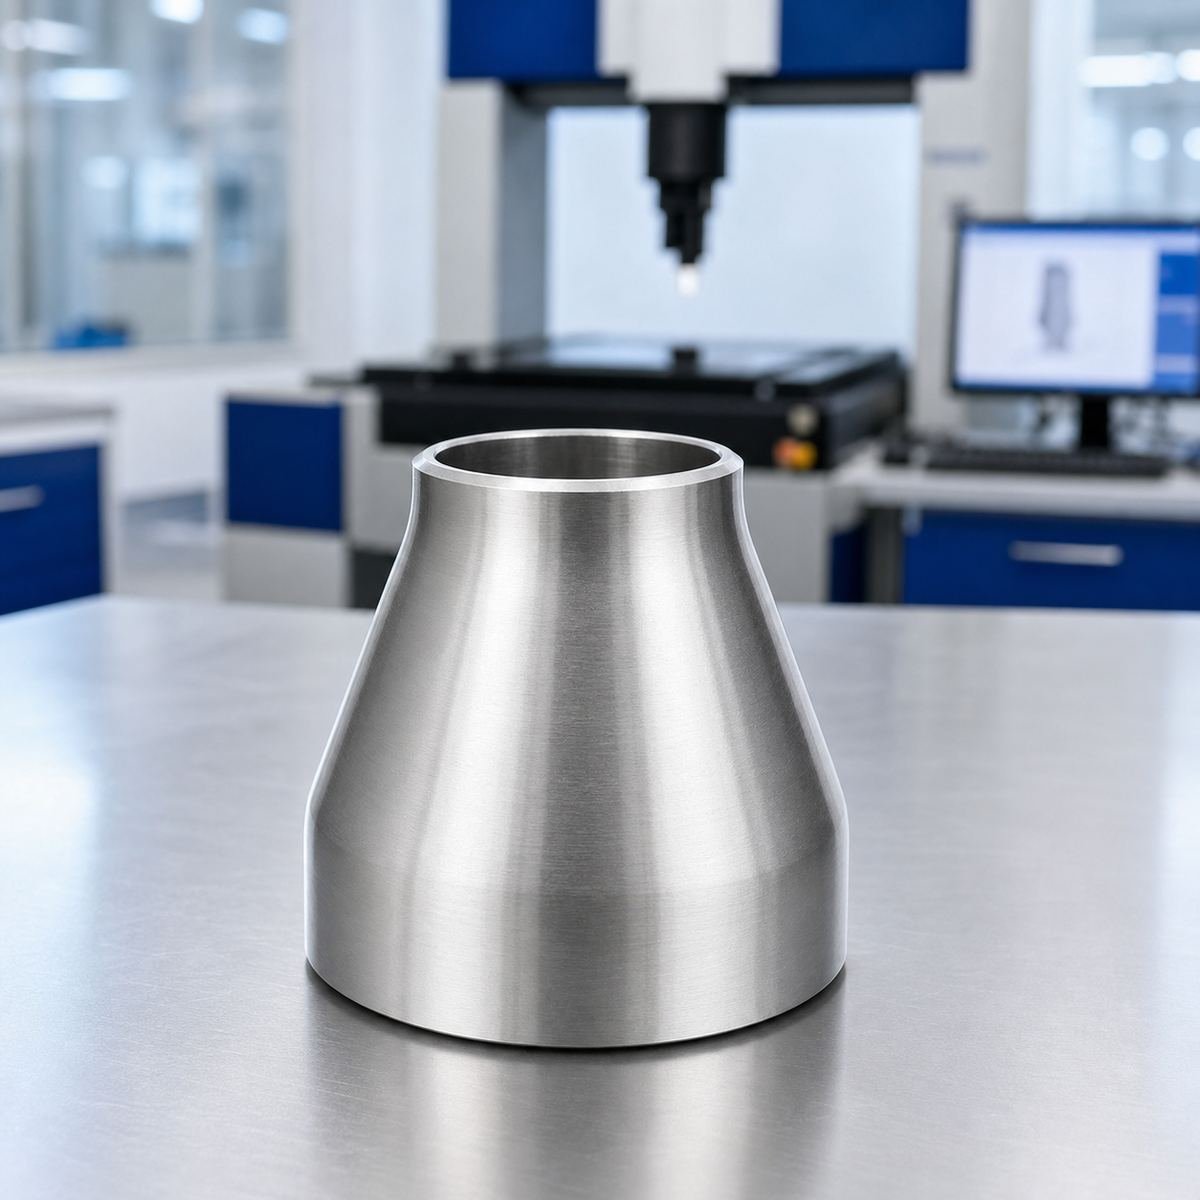
ASTM A234 WP91 Alloy Steel Concentric Reducer
A procurement-ready concentric butt-weld reducer in ASTM A234/A234M WP91 9Cr-1Mo-V-Nb alloy steel, supplied for advanced high-temperature steam and power piping with project-defined dimensions, wall, construction and inspection.
What is a WP91 alloy steel concentric reducer?
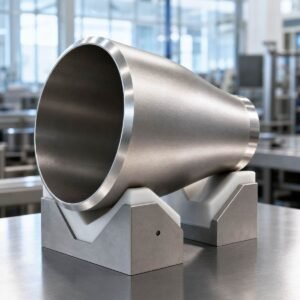
A concentric reducer provides a symmetrical change between two pipe diameters. It is widely used in vertical lines, pump discharge, process headers and services where maintaining a common centerline is appropriate.
WP91 is used in selected high-temperature power and process systems where its creep-strength-enhanced metallurgy is required. Manufacturing, welding, repair, heat treatment, hardness and records must be controlled as a complete system.
Technical specification
| Product type | Concentric butt-weld reducer |
|---|---|
| Material | ASTM A234/A234M WP91 9Cr-1Mo-V-Nb alloy steel |
| Material family | Creep-strength-enhanced ferritic alloy steel |
| Dimensional basis | ASME B16.9 or approved project drawing |
| Configuration | Concentric transition; larger and smaller ends on a common centerline |
| Nominal size | Standard ASME combinations and custom large/small-end combinations subject to review |
| Wall thickness | Standard schedules, heavy wall and project-specific wall subject to manufacturing review |
| Construction | Seamless or welded as applicable, ordered and permitted by the material class |
| End preparation | Butt-weld bevel matched to connecting pipe wall and approved welding detail |
| Heat treatment | Strictly controlled to ASTM A234 WP91 and project CSEF requirements |
| Documentation | EN 10204 3.1 MTC, heat traceability, PMI, dimensions and additional NDE as ordered |
Available size and wall combinations depend on alloy, forming route, construction and quantity. Confirm the exact pipe outside diameter and wall in the RFQ.
Standards and technical references
Dimensional standard
ASME B16.9 covers standard factory-made wrought butt-weld reducer dimensions, tolerances, marking and related requirements.
Material specification
ASTM A234/A234M includes wrought alloy steel fitting grades for elevated-temperature service; WP91 requires careful CSEF controls.
Why select WP91?
WP91 is considered for main steam, hot reheat and other advanced high-temperature services that explicitly specify P91/WP91 material systems.
| Selection point | WP91 | WP22 |
|---|---|---|
| Material family | CSEF 9Cr-1Mo-V-Nb | Conventional 2.25Cr-1Mo |
| Fabrication control | Very demanding heat treatment and hardness control | Controlled Cr-Mo fabrication |
| Typical duty | Advanced high-temperature steam systems | High-temperature steam/process systems |
| Substitution | Never without full engineering review | Never without engineering approval |
Typical applications
| Industry | Typical fitting duty | Why this material is considered |
|---|---|---|
| Thermal power | Diameter transition in vertical or centerline-aligned process piping | Main steam and hot reheat systems where specified |
| Power boilers | Equipment and header connection between different pipe sizes | High-temperature boiler and turbine-associated piping |
| Process plants | Welded size reduction where a compact transition is required | Special elevated-temperature CSEF material classes |
Application examples are selection context, not a design approval. Confirm process chemistry, pressure, temperature, weld procedure and governing code.
Manufacturing, inspection and documentation
Reducer manufacture requires control of end diameters, overall length, wall transition, ovality, concentricity and bevel geometry. WP91 orders should define full heat-treatment records, hardness mapping, weld-repair controls, NDE and any project-specific CSEF acceptance criteria.
Heat-number traceability and PMI when specified.
Large/small-end OD, wall, length, concentricity, ovality and bevel checked.
PT, MT where applicable, UT, RT or third-party witnessing to the ordered scope.
MTC, heat-treatment and inspection records compiled to project requirements.
RFQ checklist
- Complete material grade and UNS where applicable
- ASME B16.9 edition or approved project drawing
- Run, outlet and branch sizes
- Schedule or exact wall thickness at every end
- Seamless or welded construction/class
- Bevel detail and matching pipe dimensions
- Quantity, destination and required delivery date
- EN 10204 3.1, PMI, dimensional and NDE requirements
Frequently asked questions
What is a WP91 alloy steel concentric reducer?
It is a Concentric butt-weld reducer manufactured from ASTM A234/A234M WP91 9Cr-1Mo-V-Nb alloy steel. Its large and small ends share one centerline, producing a symmetrical transition. The ordered material specification controls chemistry, mechanical properties, heat treatment and testing.
Which standard applies to this fitting?
ASME B16.9 covers standard factory-made wrought butt-weld reducer dimensions, tolerances, marking and related requirements. The material basis is ASTM A234/A234M WP91 9Cr-1Mo-V-Nb alloy steel. The purchase order must state the required edition, construction, size, wall and supplementary examinations.
Where is WP91 typically selected?
WP91 is considered for main steam, hot reheat and other advanced high-temperature services that explicitly specify P91/WP91 material systems. Material suitability still depends on fluid chemistry, pressure, temperature, fabrication, corrosion allowance and the governing piping code.
Can heavy-wall and welded construction be supplied?
Yes, subject to manufacturing review. Provide the exact outside diameter, wall thickness or schedule, construction class, end preparation, quantity and NDE requirements so feasibility can be confirmed.
What should an RFQ include?
State the complete material grade, dimensional standard or approved drawing, run and branch sizes, schedule or exact wall, seamless or welded construction, bevel detail, quantity, destination, certification and inspection scope.
Product image is representative. Surface appearance varies by alloy, manufacturing route and finish.
Request a technical quotation
Send the material, size combination, wall, quantity, drawing or standard, and inspection requirements for review.