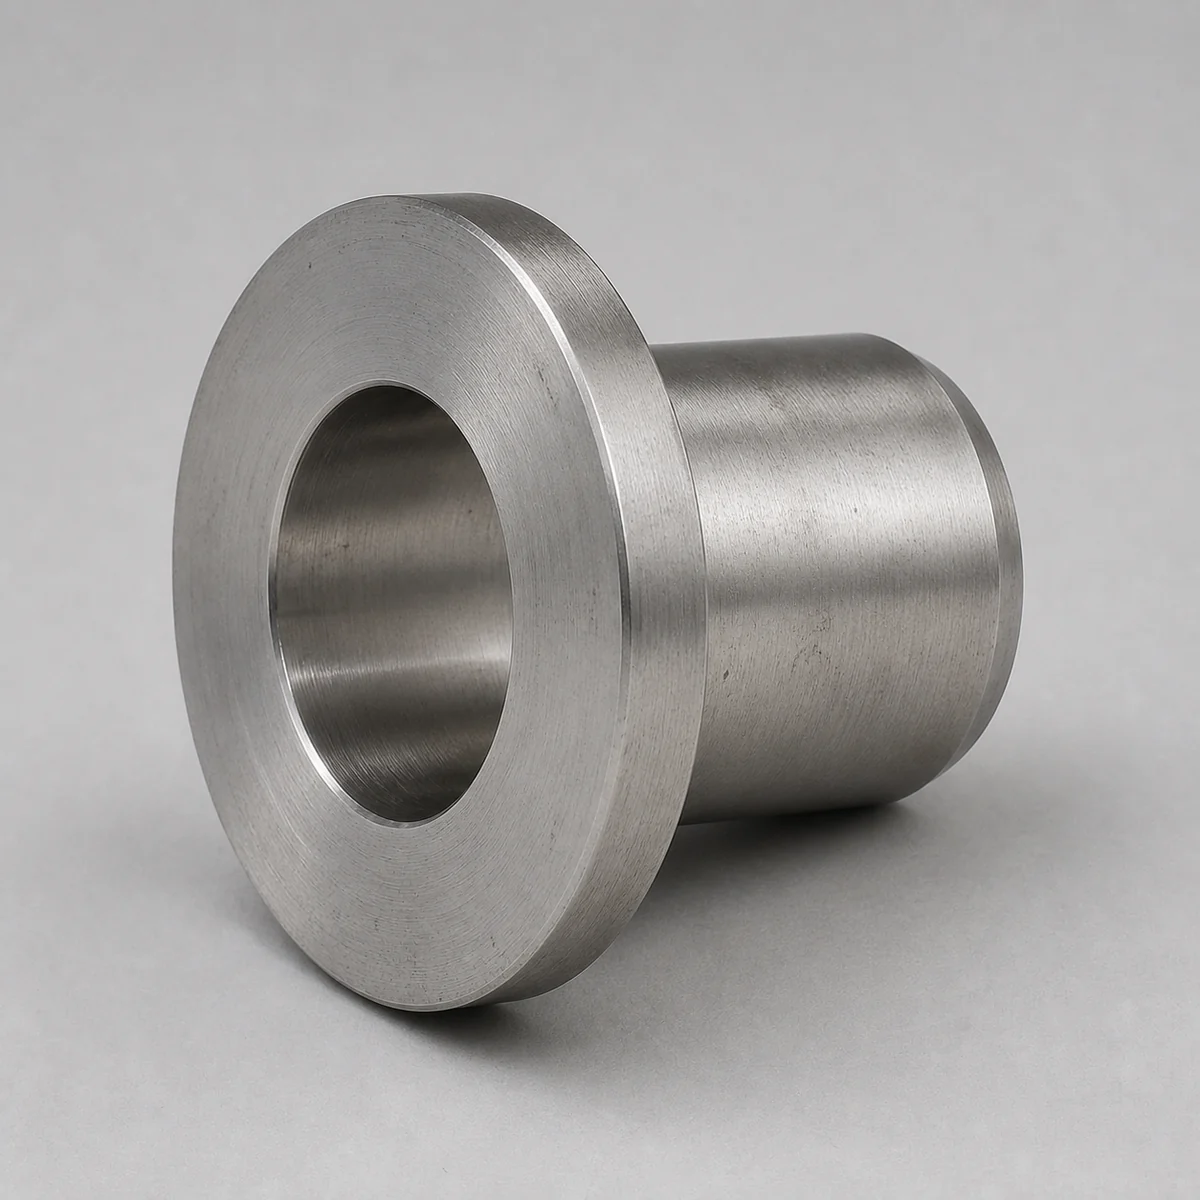
Description
Lap-joint butt-weld fitting | ASME B16.9 / MSS SP-43
ASTM A815 S32750 Super Duplex 2507 Stub End
Lap-joint stub end in ASTM A815 WP-S32750 Super Duplex 2507 for demanding chloride piping assemblies. Available with project-specific dimensions, documentation and inspection.
Direct answer
What is a Super Duplex 2507 stub end?
A stub end is a butt-weld piping fitting used with a loose lap-joint backing flange. The stub end provides the process-wetted sealing face and weld connection, while the backing flange rotates freely behind the lap. This arrangement can simplify bolt-hole alignment and allows the backing flange material to be selected separately when the design permits.
ASTM A815 WP-S32750 designates a seamless wrought super duplex fitting in UNS S32750. It is a product-form designation distinct from ASTM A182 F53 forgings.
The lap face, corner radius, hub length, wall thickness and weld end must suit the backing flange, gasket and connected pipe. Long-pattern and short-pattern dimensions are not interchangeable. The pressure capability belongs to the complete engineered joint, not to the stub end in isolation. The piping specification should define the material combination, corrosion allowance, weld procedure and dimensional standard.
Technical specifications
| Product | Stub End |
|---|---|
| Material specification | ASTM A815 WP-S32750 |
| UNS designation | UNS S32750 |
| Dimensional standard | ASME B16.9 / MSS SP-43 |
| Size range | Standard and project-specific sizes within the selected ASME B16.9 or MSS SP-43 dimensional range |
| Rating / schedule | Wall schedule and backing-flange rating selected for the complete lap-joint assembly |
| Configuration | Type A or specified lap-joint stub end, long or short pattern as ordered, with butt-weld end |
| Documentation | EN 10204 3.1 MTC, heat-number traceability, dimensional report and PMI when ordered |
| Optional inspection | PMI, PT, ferrite, ASTM G48 testing and third-party inspection when ordered |
Final dimensions, ratings, tests and acceptance criteria follow the purchase order, approved drawing, applicable code and specified standard edition.
Why specify Super Duplex 2507?
S32750 provides high strength and strong localized-corrosion resistance for selected seawater, offshore and chloride services. Design temperature, fabrication and project acceptance criteria still control suitability.
Weld preparation, cleanliness, heat input and interpass temperature must follow qualified super-duplex procedures. The backing flange and gasket should also be reviewed for the service environment.
Typical applications
These are selection examples, not universal suitability claims. Verify corrosion, temperature, pressure, fabrication and code requirements for the actual service.
Ordering and specification guidance
State the fitting material designation, UNS number, NPS, wall schedule, dimensional standard, pattern, lap-face requirements and mating backing flange. For nickel-alloy and duplex products, confirm whether seamless or welded construction and the applicable ASTM class marking are required.
Include the required WP class, schedule, pattern, ferrite, corrosion test and third-party inspection requirements.
Engineering selection boundaries
Material grade, nominal size and pressure class are necessary purchasing inputs, but they do not prove suitability by themselves. The responsible piping engineer should verify the design code, design pressure and temperature, corrosion allowance, connected pipe dimensions, flange facing, gasket system, bolting, welding procedure and examination plan as one coordinated specification. Service chemistry, concentration, contaminants, velocity, shutdown conditions and cleaning media can change corrosion performance. Request written confirmation against the project datasheet and approved drawing before manufacture, especially where sour service, seawater exposure, cyclic loading, vacuum, lethal service or regulatory inspection applies.
Manufacturing, inspection and traceability
Inspection covers chemistry and heat-treatment certification, wall thickness, lap outside diameter, face thickness, corner radius, overall length, weld-end preparation and surface condition. PMI and PT can be specified for corrosion-resistant alloys.
PMI, ferrite measurement and ASTM G48 testing can be specified alongside routine dimensional and visual inspection.
Official standards and engineering references
Use the current project-approved editions. The following official scope pages help procurement teams separate dimensional requirements from material requirements.
Related stub end products
RFQ checklist
- ASTM grade and UNS designation
- NPS and pipe schedule
- ASME B16.9 or MSS SP-43
- Long or short pattern
- Type and lap-face dimensions
- Backing-flange material and class
- Seamless or welded construction
- MTC, PMI, PT and inspection
Frequently asked questions
Does a stub end include the backing flange?
Not unless the purchase order states it. A stub end and a lap-joint backing flange are separate components and may use different material specifications.
What is the difference between long-pattern and short-pattern stub ends?
They have different overall lengths and assembly considerations. The required pattern must be stated and matched to the project dimensional standard.
Can a carbon steel backing flange be used with an alloy stub end?
It can be considered when the design, environment, corrosion protection, temperature and piping code allow it. The project engineer must approve the material combination.
Is ASTM A815 S32750 the same as ASTM A182 F53?
They refer to the same UNS alloy family but different product forms. A815 covers wrought fittings; A182 F53 covers forged components.
Should the ASTM A815 class suffix be specified?
Yes. The WP-S, WP-W, WP-WX or WP-WU suffix communicates construction and examination requirements.
Request a technical quotation
Send the material grade, standard, size, rating or schedule, quantity and inspection requirements. SASA FLANGE will review the complete specification before quotation.